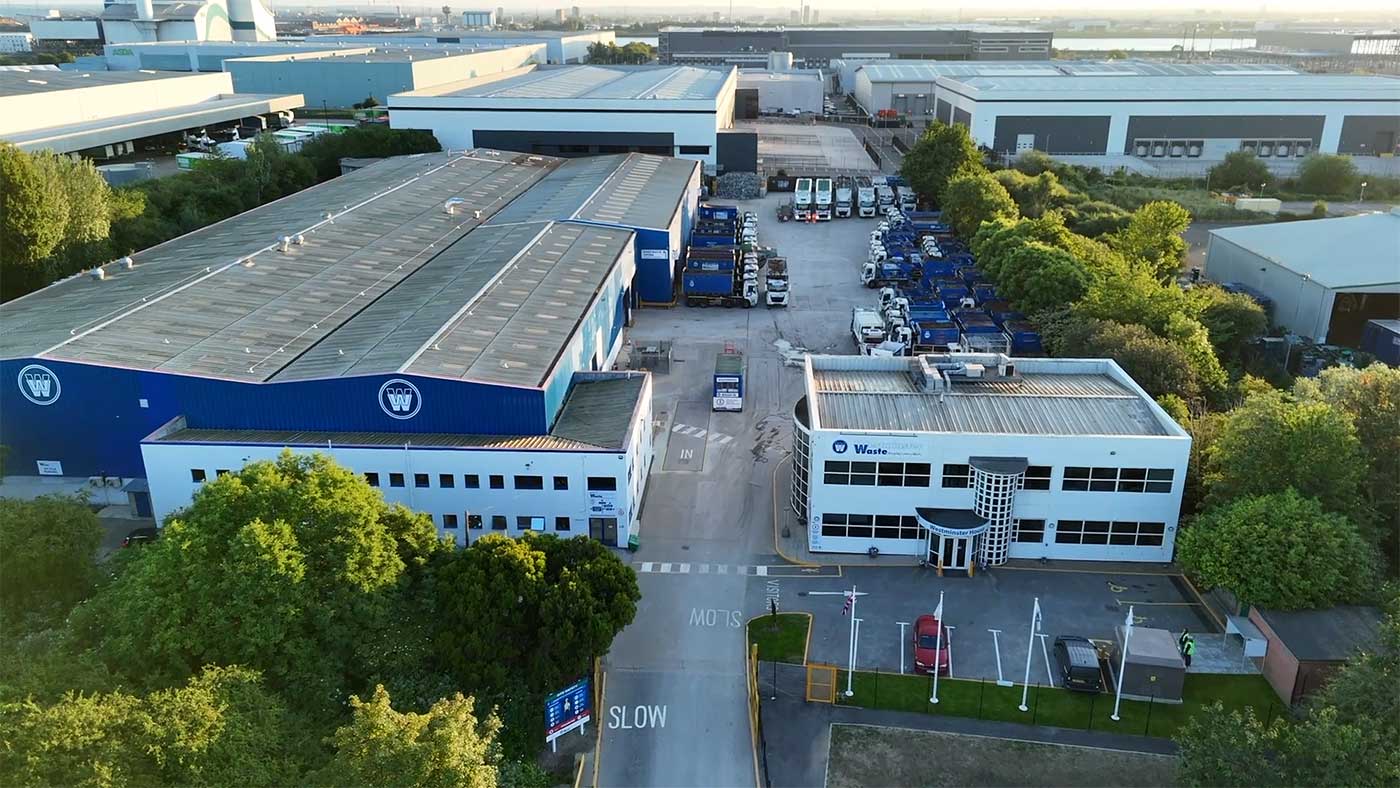
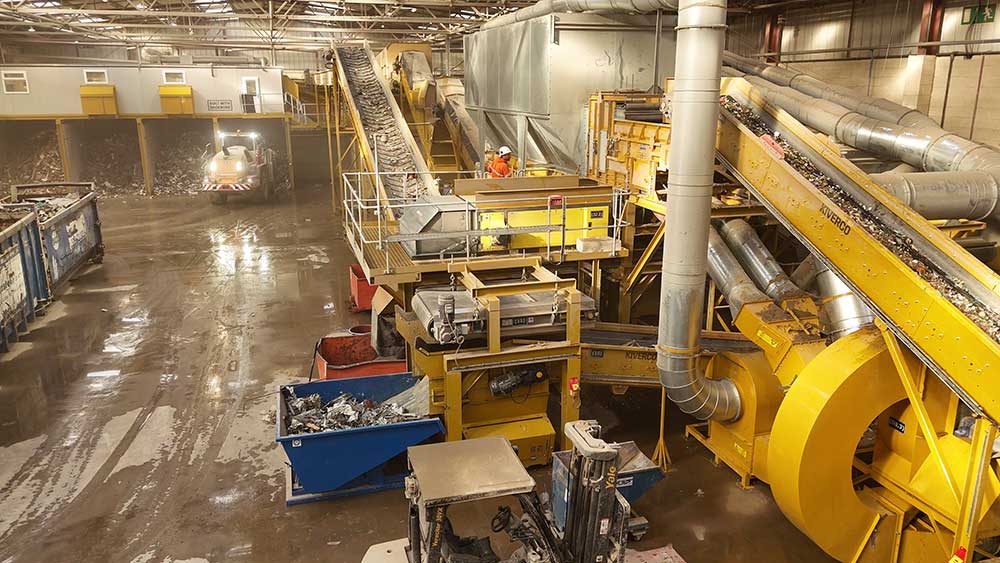
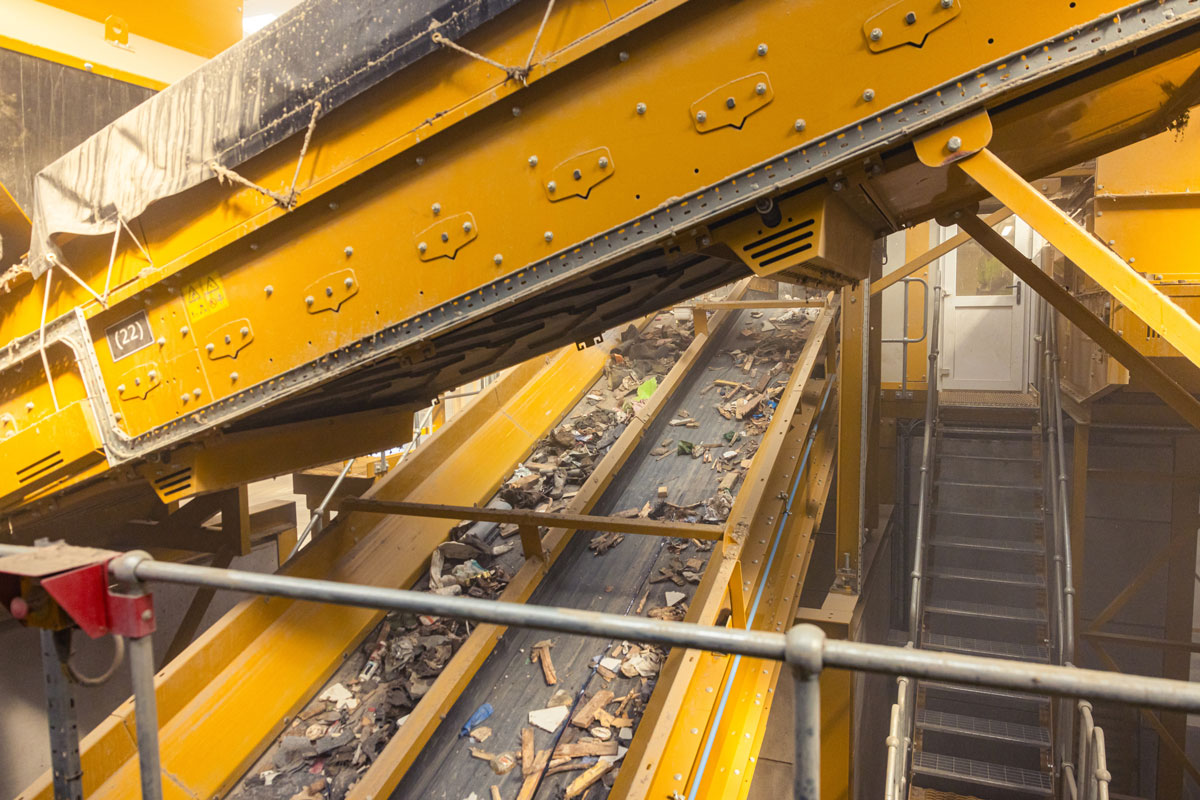
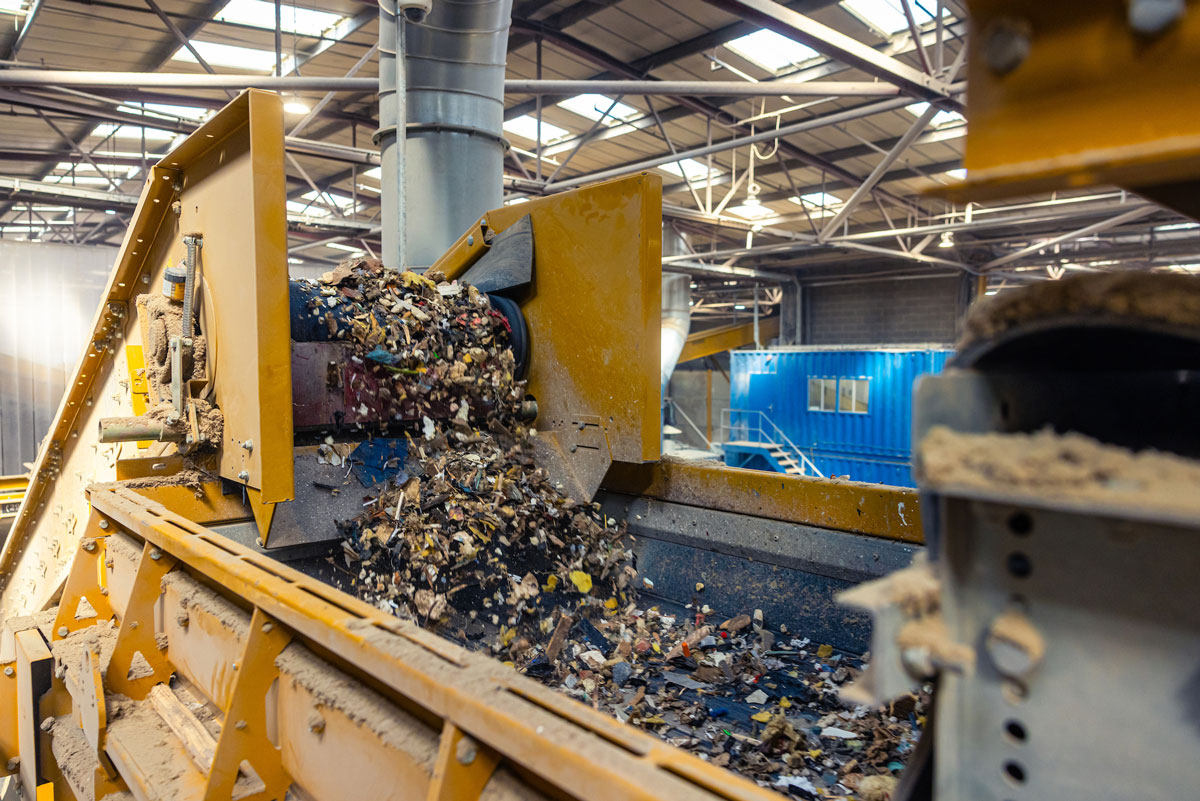
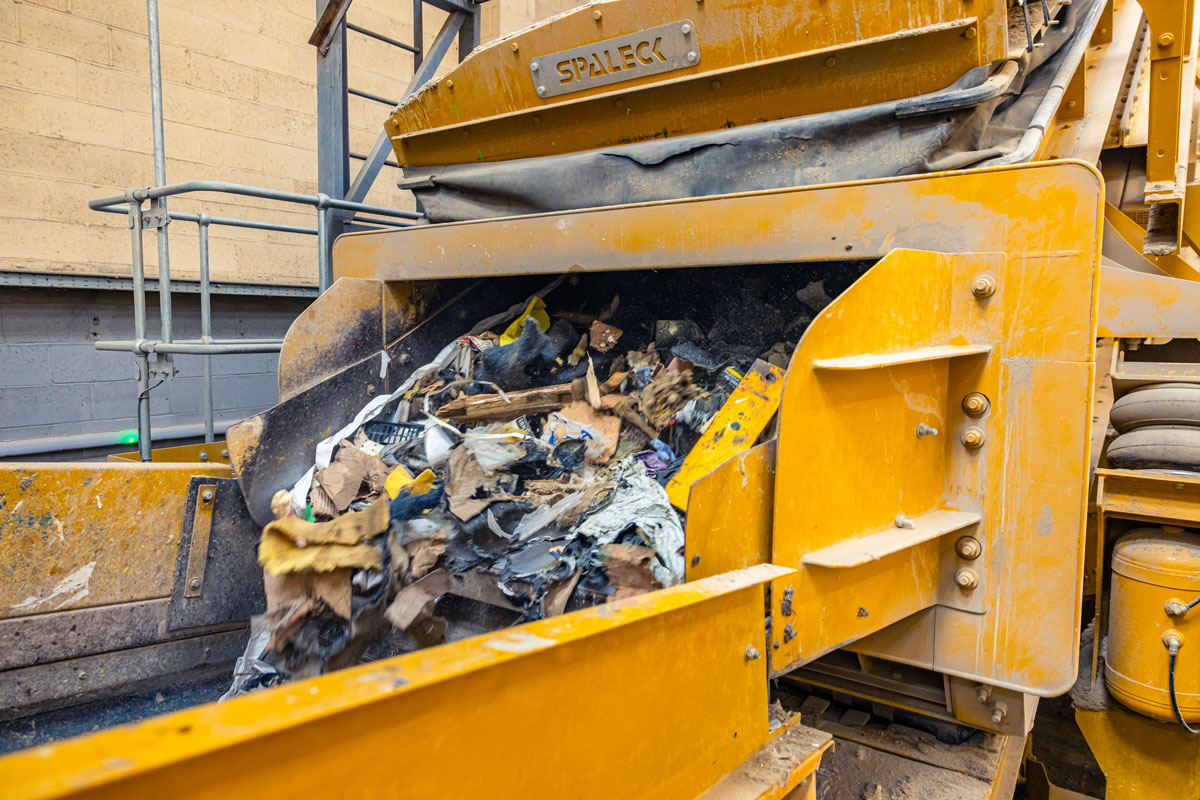
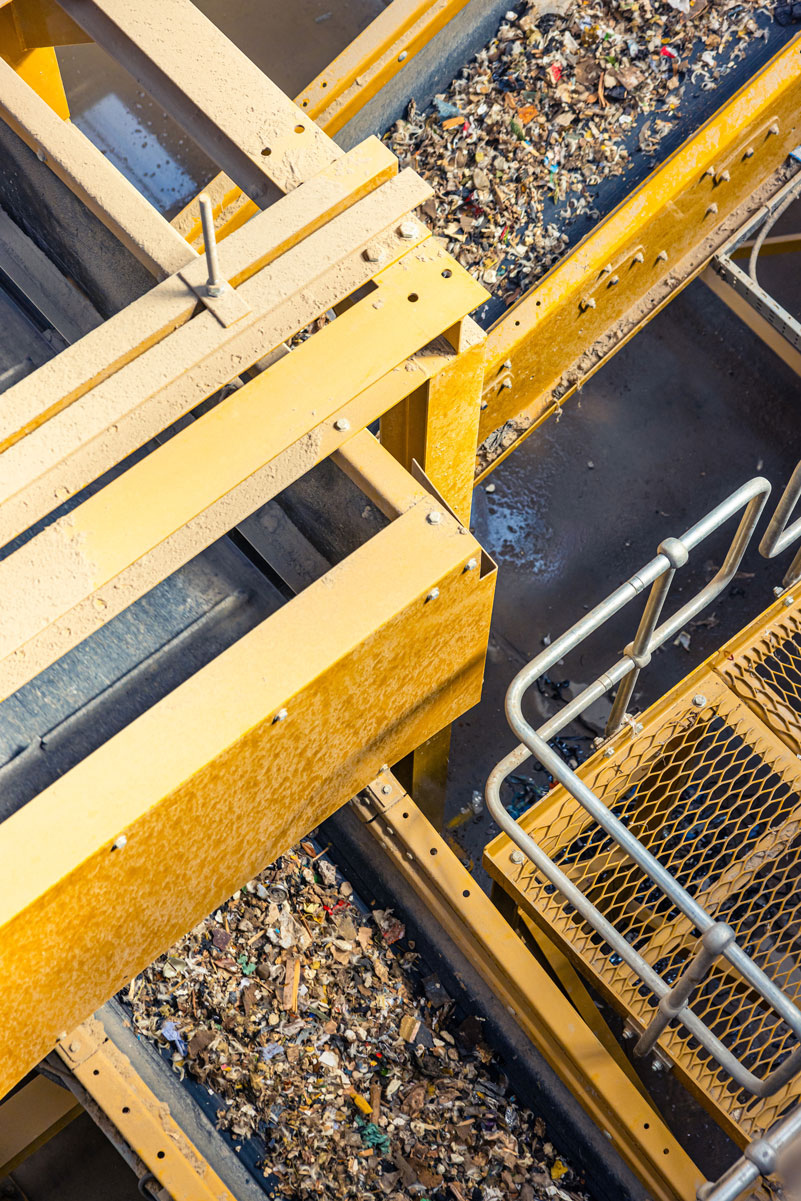
A multi-million-pound facility — one of the largest of its kind in South East England, processing up to 60 tonnes per hour ensuring 100% landfill diversion.
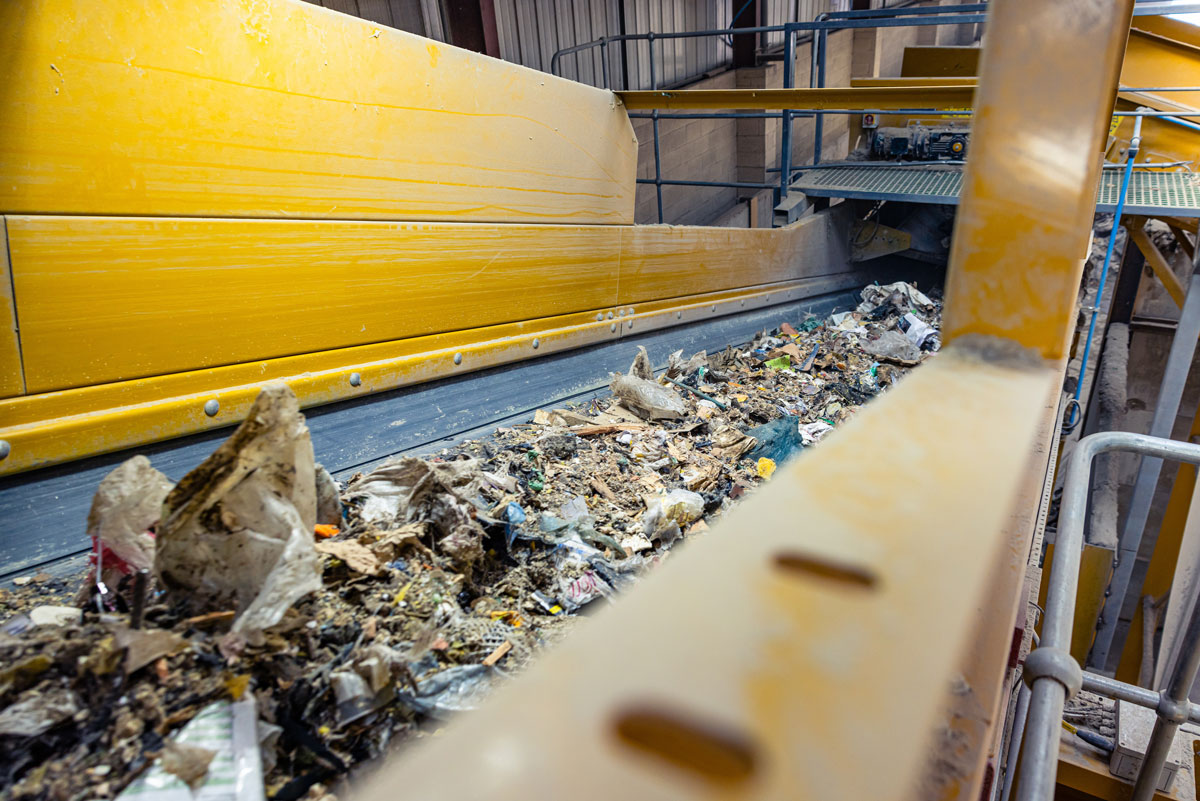
Our Material Recovery Facility (MRF) is one of the few facilities of its kind in the South East. It allows us to secondary sort mixed waste materials to extract single-stream recyclate, pushing volume up the waste hierarchy and boosting the recycling rates of our customers.
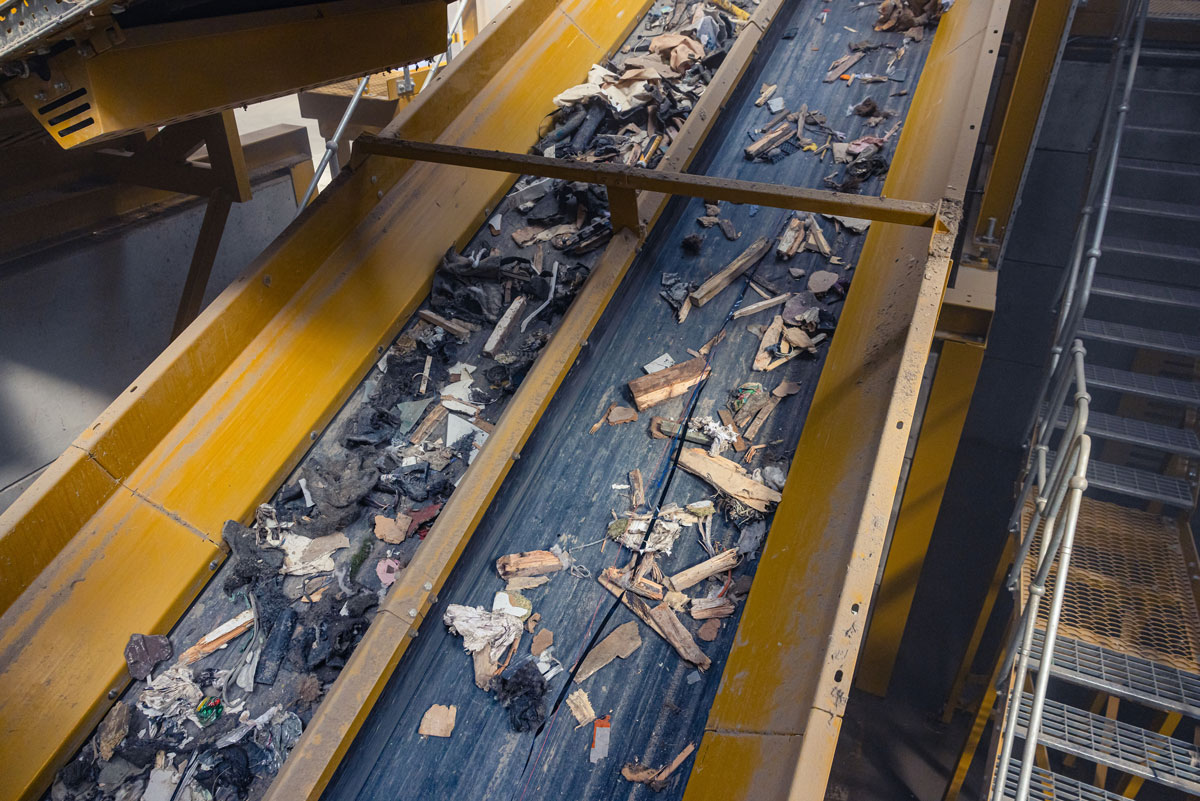
The facility is engineered to handle three distinct waste streams: Construction and Demolition (C&D), Commercial and Industrial (C&I), and Wood. The main objectives were to achieve 100% landfill diversion, increase throughput to 60 t/hr, improve purity of recovered materials, and reduce reliance on manual labour.
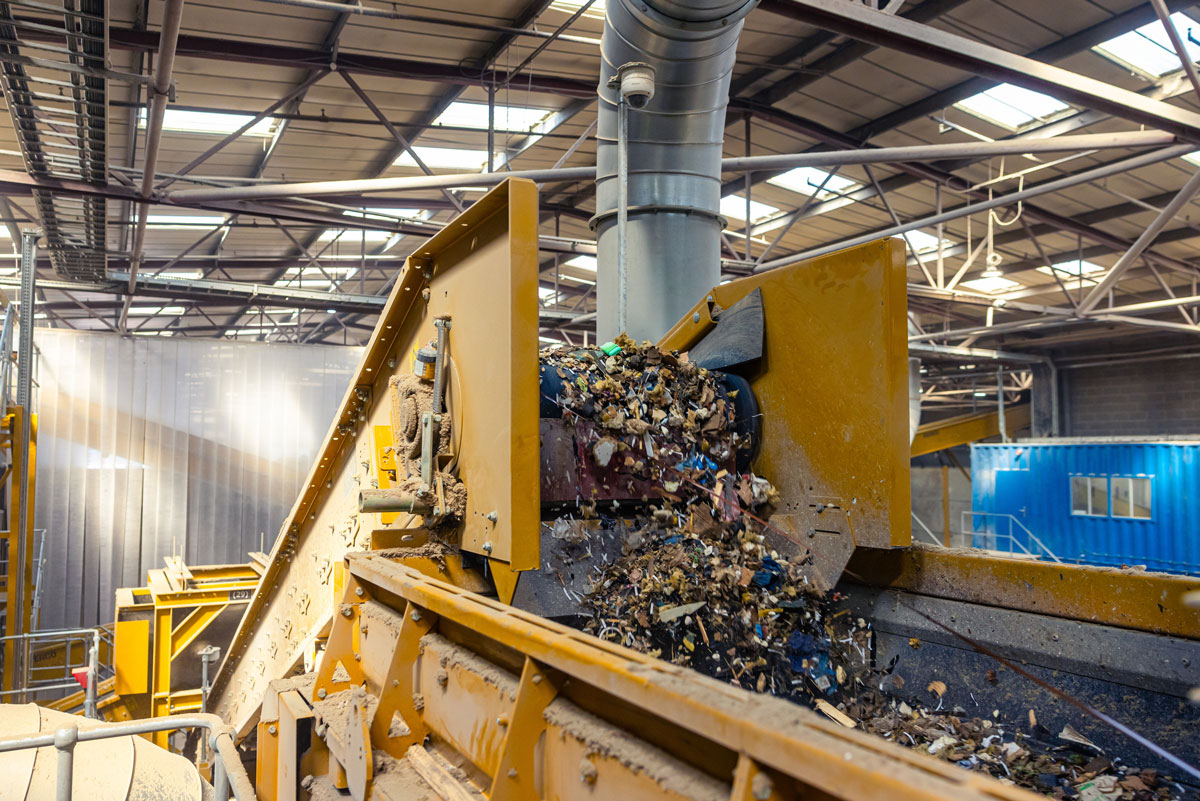
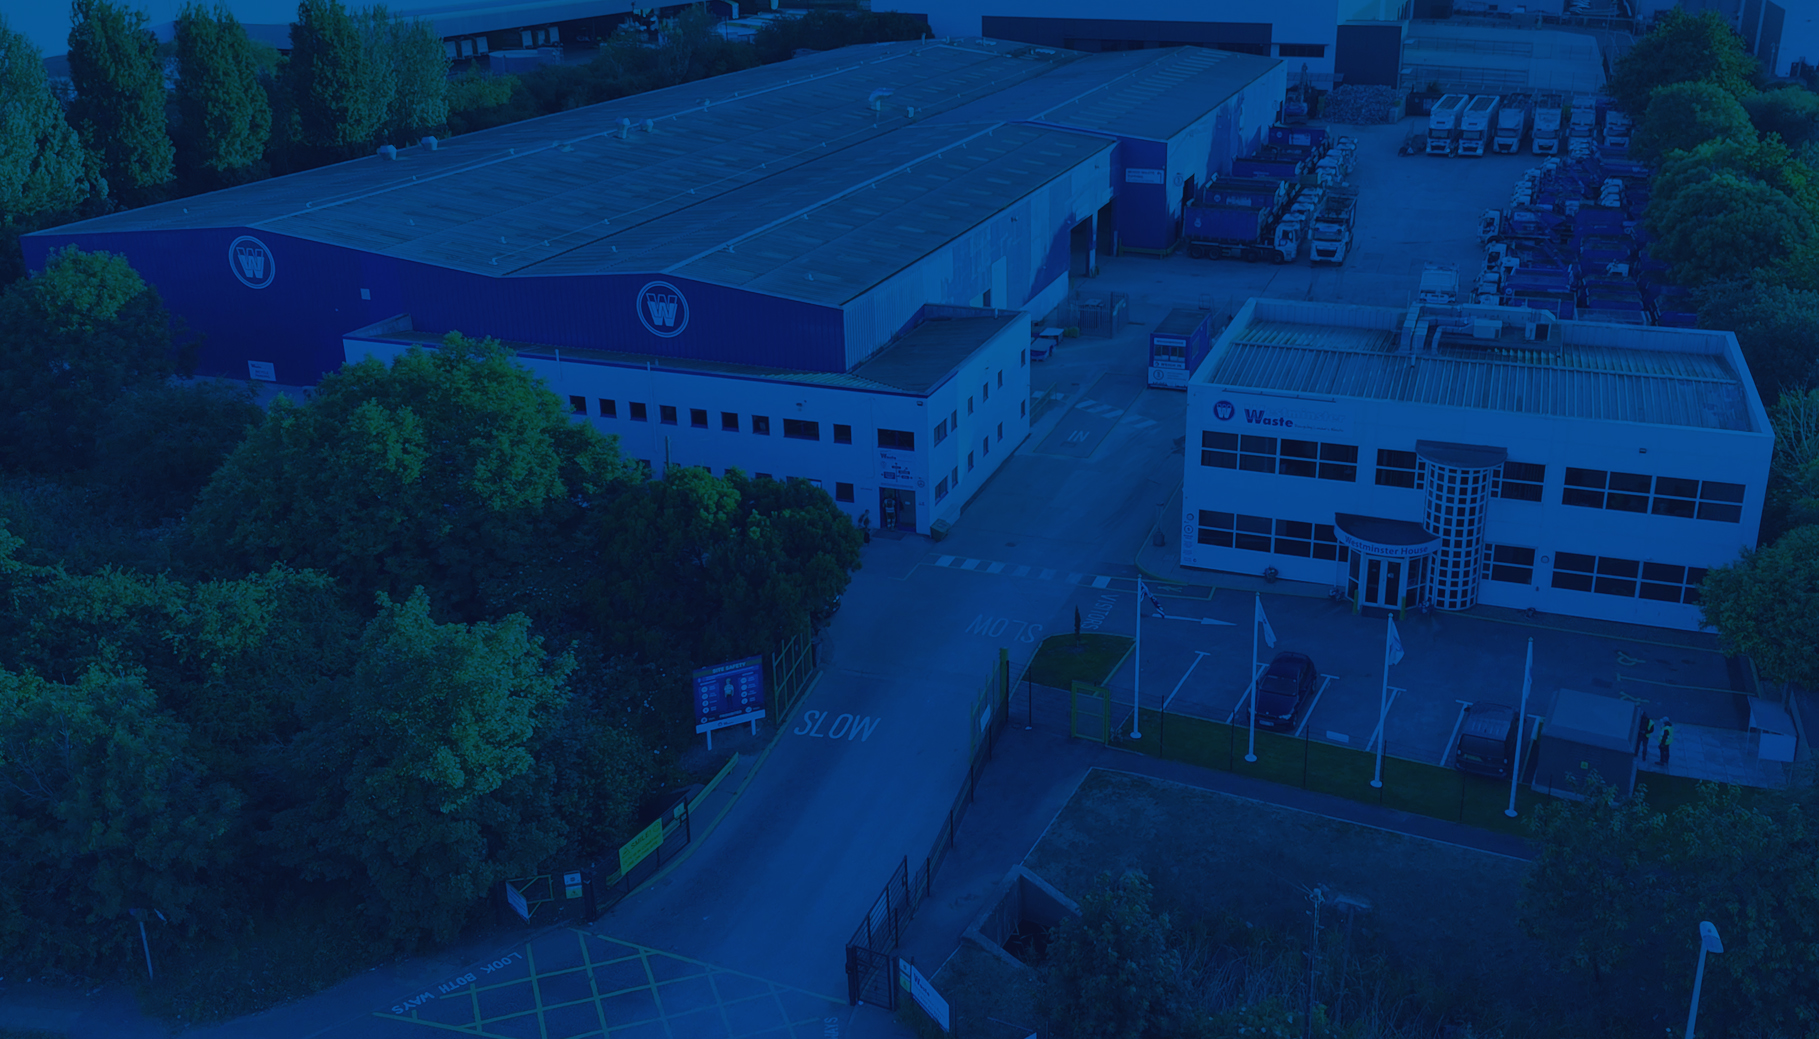
Integrating advanced automation technologies was crucial to optimise waste separation and maximise operational capacity at our site in Belvedere.
Multi-million-pound investment commissioned 2024
One of the largest facilities of its kind in South East England
Designed to handle high-bulk-density C&D waste
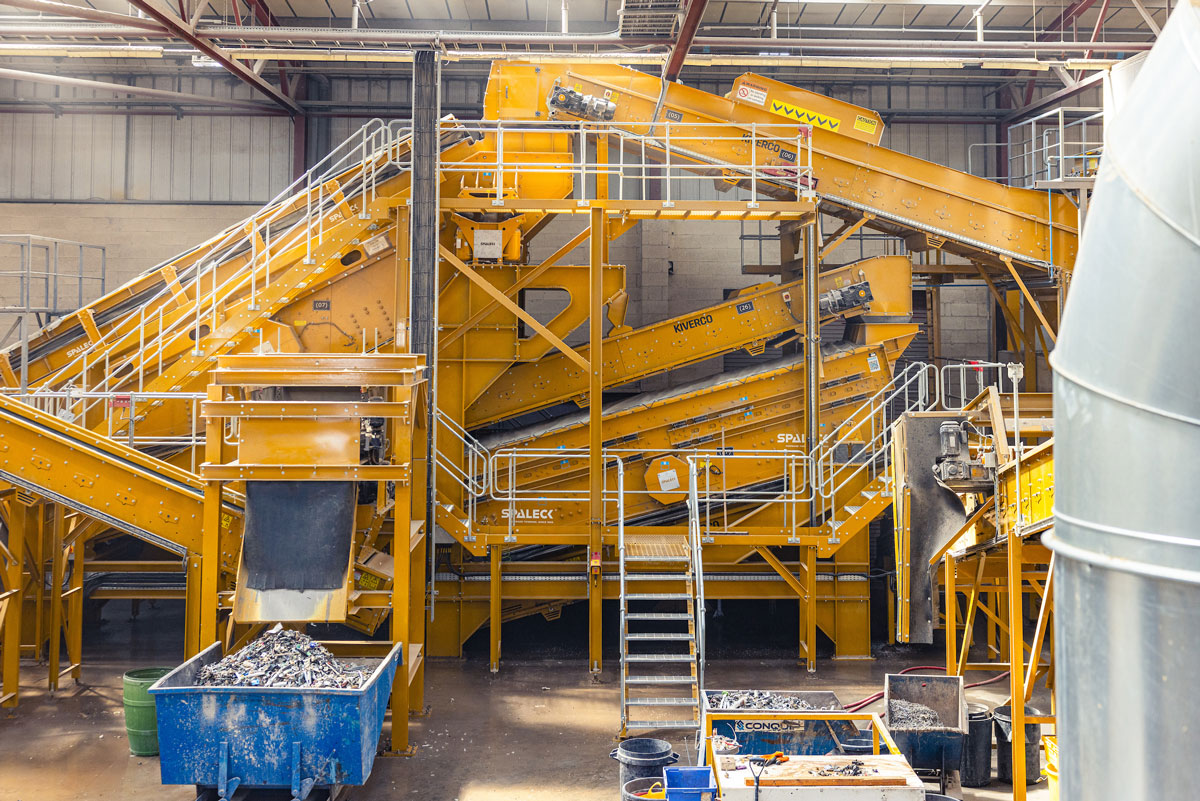
Advanced automation: NIR optical sorters, eddy current, magnetic separation
Fully adaptable for future waste stream growth
Recovered metals processed through approved recycling partners
Member of the Wood Recyclers Association
EA licensed facility — fully auditable chain of custody
60t
PER HOUR
100%
DIVERTED FROM LANDFILL
The Sorting Line
How the MRF Works
Advanced sorting reduces contamination, raises purity and lifts throughput well above manual lines.
Step by Step
01 Primary Screen
In-feed conveyor screens by size. Oversized C&D fractions break down; fines peel off for aggregate.
02 Ferrous Separation
Overhead magnetic drums extract steel and iron at high throughput, clean and at purity.
03 Eddy Current
Non-ferrous metals — aluminium, copper, brass — ejected by eddy-current at line speed.
04 NIR Optical Sorting
Near-infrared sorters identify and eject individual plastic grades, paper, card and wood.
05 Quality Assurance Cabin
A final quality-check cabin removes contaminants before baling — ensuring clean single-stream output.
06 Bulk & Dispatch
Materials once separated are bulked and sent for onward recycling and processing. Recycling reports are auto generated.
The MRF accepts mixed loads and separates them into clean recyclate. Every stream has a recovery pathway — nothing goes to landfill by default.
C&D
Construction & Demolition
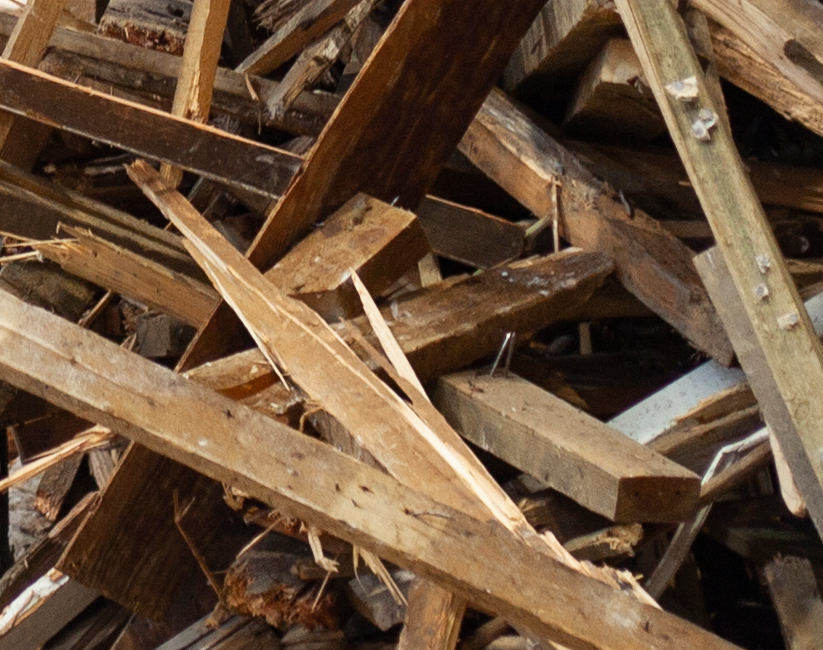
Rubble, bricks, concrete, timber — the highest-bulk-density stream the plant is specifically engineered to handle.
C&I
Commercial & Industrial
Mixed commercial waste collected from offices, retail, hospitality and industrial facilities is processed through advanced automated sorting.
WOOD
Wood Recycling
Clean and mixed waste timber is separated, graded and processed into high-quality recycled wood products, supporting a sustainable circular economy.
METALS
Metals Recovery
Powerful magnets and eddy current separators recover ferrous and non-ferrous metals with high purity before dispatch to approved recycling partners.
RECYCLABLES
Plastic & Paper
Advanced NIR optical sorters identify plastics, cardboard and paper, producing clean recyclable streams for further processing.
RESIDUAL
Energy Recovery
After recyclable materials are removed, the remaining residual fraction is processed into alternative fuel, helping achieve landfill diversion targets.
"This new plant represents a huge leap forward for our business. Our goal has always been to lead the way in sustainable waste management, and with this facility, we're well on our way to achieving 100% diversion from landfill."
Every tonne you send to Westminster Waste is processed through our MRF. Your waste gets a recycling report, a weighbridge ticket, and a Waste Transfer Note — and your recyclable rate goes up.